2026 Best CNC Machinist Services for Global Buyers?
Choosing a CNC machinist for an international project is not just a search for the lowest unit price. Buyers need consistent dimensions, dependable inspection, clear communication, and realistic delivery dates. A small variation in a bore or thread can affect assembly far more than a polished sales page suggests. Details matter.
This guide explores how global buyers can compare machining services in 2026, from material expertise and machine capacity to quality records and engineering support. Review whether a supplier can explain tolerances, surface finishes, inspection methods, and what its quotation excludes. Ask for relevant part examples, sample reports, and a clear plan for changes after drawing approval. Good answers are specific. Vague promises deserve follow-up.
For cross-border orders, compare lead times, packaging, freight terms, response windows, and how defects or delays are handled. Confirm applicable quality certifications directly, and check that their scope matches your parts. A supplier may have advanced equipment, yet still struggle with documentation or a rushed schedule. Not every supplier fits.
Rather than presenting one shop as best for every buyer, this overview offers practical criteria for building a shortlist and asking sharper questions. A scorecard helps, but cannot capture every shop-floor surprise. That limitation is worth remembering. With careful checks, buyers can balance price, precision, communication, and delivery before committing to production.
What CNC Machinist Services Do Global Buyers Need in 2026?
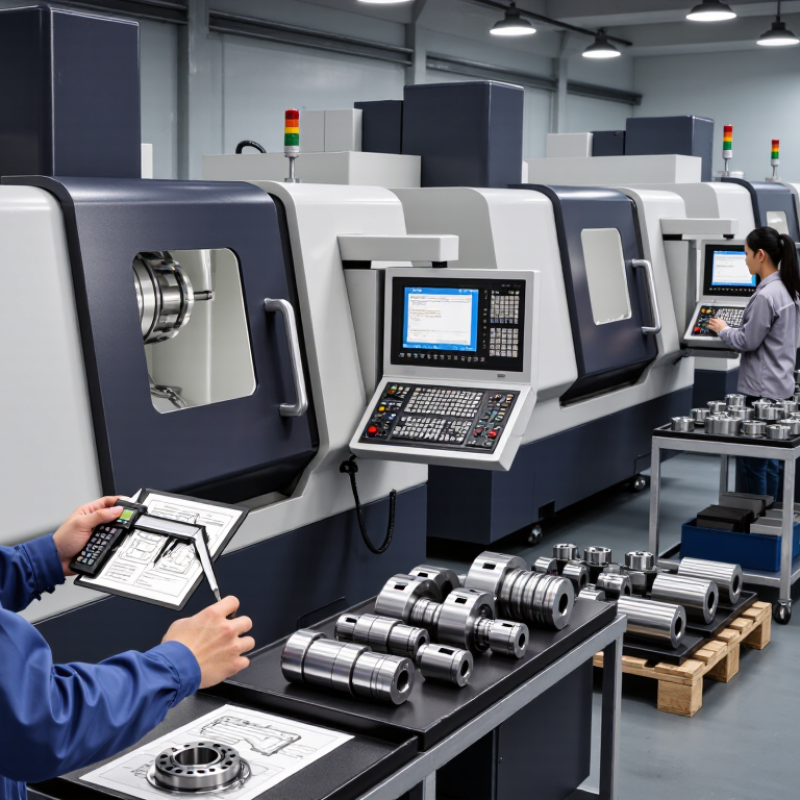
Global buyers need more than a machine that can cut metal. They need CNC machining services that turn drawings into repeatable parts, with clear communication across time zones. A capable shop reviews tolerances, datum choices, wall thickness, and tool access before quoting. That matters. A deep pocket with a sharp internal corner, for example, may require a design adjustment or an extra setup. Small details count.
Buyers may need milling, turning, drilling, prototyping, and production runs, along with finishing and inspection. Material traceability can be important too, especially when parts must match a specified alloy or grade. Ask for a first-article inspection report, dimensional records for critical features, and clear notes on any deviations. These checks help catch a hole that is slightly misplaced before hundreds of parts are made.
Shipping coordination and responsive updates are part of the service, not an afterthought. A useful RFQ includes the 3D model, drawing revision, quantity, target delivery date, and critical dimensions. One weakness in many requests is assuming every tolerance matters equally; that can raise cost without improving function. Not every time. Buyers should still confirm packaging, lead-time assumptions, and how design changes will be handled, since those details can become unclear once production starts.
How to Specify Tolerances Using ISO 2768 and ISO 286
A clear tolerance scheme helps a CNC machinist choose tools, inspection methods, and a realistic process. ISO 2768 provides general tolerances for dimensions without individual limits. State the applicable class on the drawing, such as “ISO 2768-mK,” and identify the standard edition. In this notation, “m” covers general linear and angular tolerances; “K” covers general geometrical tolerances. Check the relevant tables before relying on either class. They do not replace tolerances on critical features.
Use ISO 286 when a cylindrical feature needs a defined fit. Its hole-and-shaft system uses letters for tolerance-zone position and numbers for tolerance grade. For example, H7/g6 describes a specific hole-and-shaft combination, not a universal clearance. Confirm the nominal diameter and consult the applicable ISO 286 tables before releasing the drawing. That matters. A bearing seat, locating pin, and free-sliding sleeve may need different fits.
Make the functional requirement visible. A 20 mm shaft entering a reamed bore should show its individual size limits or fit designation, plus relevant surface and geometric controls. Identify datums when position or runout matters, and state how the feature will be inspected. Avoid applying fine tolerances to every dimension; they can raise machining and measurement demands without improving function. Measure it. One detail is easy to miss: temperature and measurement setup can affect close-fit inspection, so agree on a method before production begins.
How to Compare Materials, Inspection, and Lead-Time Capabilities
A CNC quote is only comparable when the material, inspection plan, and delivery clock are clear. Ask for the exact alloy and temper, not simply “aluminum” or “stainless steel.” A supplier should confirm stock availability, machining tolerances, surface finish, and whether parts need heat treatment or outside processing. For inspection, request a sample dimensional report tied to drawing revision, plus details on calibrated instruments and first-article checks. Ask which features are measured on every part. Small holes and thin walls can need different controls.
Lead time needs the same detail. Request separate estimates for material procurement, machining, inspection, and shipping, with the quote’s start point stated. The World Bank’s 2023 Logistics Performance Index assessed 139 economies across six dimensions, including timeliness and shipment tracking. That is a useful reminder: factory capacity alone does not predict arrival dates. McKinsey’s 2022 supply-chain survey found 45% of respondents lacked visibility beyond tier-one suppliers, making outsourced finishing and material sourcing worth checking. Ask whether the quoted schedule includes these steps, and what triggers a revised date. A neat spreadsheet can still hide a weak assumption. I would ask for a recent example of a comparable job, while recognizing that one example cannot guarantee the next delivery.
How to Qualify Global Suppliers: ISO 9001:2015 and AS9100D
2026 Best CNC Machinist Services for Global Buyers?
How to Qualify Global Suppliers: ISO 9001:2015 and AS9100D
A certificate is a starting point, not proof that every machined part will meet specification. ISO’s 2023 Survey recorded 1,265,216 ISO 9001 certificates across 189 countries and economies. That scale makes certificate checks essential. Confirm the issuing body, expiry date, and certified site. Then compare the certificate’s scope with the actual work, such as five-axis milling or tight-tolerance turning.
AS9100D builds on ISO 9001:2015 with additional aerospace quality requirements, including stronger controls for risk, traceability, and supplier oversight. Ask for records tied to your part: material certificates, inspection results, calibration status, and change approvals. Check the supplier’s AS9100D status in the IAQG OASIS database. Check the details. A certificate held by one facility may not cover another facility producing your order.
During a shop review, follow one component from incoming stock to final inspection. Look for clear lot identification, current calibration labels, and measurements recorded against the drawing—not just a polished procedure manual. Still, paperwork can miss daily practice. Ask how a machinist handles an out-of-tolerance reading, and request a redacted corrective-action example. The answer may reveal more than the certificate.