7 Best CNC Plastic Materials for Global Buyers?
Choosing the right cnc plastic is rarely a simple catalog decision. A part may look perfect on a screen, yet warp beside a warm motor or crack around a tight fastener. Global buyers must assess load, temperature, moisture, chemical exposure, tolerances, and production volume together.
Professor Tim A. Osswald, a respected polymer-processing expert, describes polymer processing as “the art and science of transforming polymers into useful products.” That idea matters in CNC machining. Material behavior changes during cutting. Tool sharpness, chip removal, heat control, and grain direction can affect the final part. A low-cost sheet can become expensive after repeated rework.
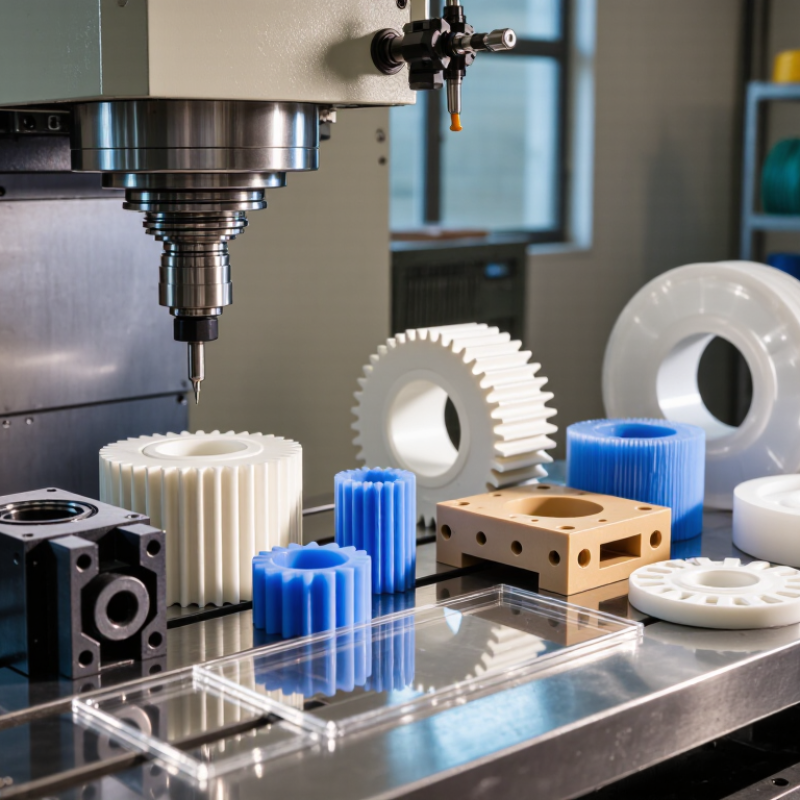
This guide examines seven widely used materials: ABS, POM, nylon, polycarbonate, PEEK, PTFE, and UHMW-PE. Each offers a different balance of strength, friction, stability, machinability, and price. POM may deliver clean, accurate gears. Nylon can handle wear, but moisture may alter its dimensions. PEEK performs in demanding environments, although its price can challenge smaller budgets. PTFE slides smoothly, yet its softness requires careful design.
Specifications are useful. Real application details matter more. Certification, traceability, and supplier process control also deserve attention across international projects. The “best” cnc plastic is not universal. It depends on the part’s actual duty, manufacturing route, and acceptable risk. Some recommendations may still need testing. That is the honest limitation. A prototype tested under real temperature, load, and humidity often reveals what a datasheet cannot.
Set Selection Criteria: Tensile Strength, HDT, Density, and ISO 2768
7 Best CNC Plastic Materials for Global Buyers
Choosing CNC plastic starts with the part’s working conditions, not a popular material list. Common options include
POM,
PA,
PEEK,
PTFE,
UHMW-PE,
ABS, and
PC. Compare tensile strength with the expected load, thread stress, and clamping force. A strong material can still crack around sharp internal corners. I have seen this mistake delay otherwise simple assemblies.
Heat changes the decision. Check the heat deflection temperature (HDT) against the highest continuous temperature, not only the room temperature.
POM suits many precision parts, while
PEEK handles demanding heat and chemical exposure.
PA offers toughness, but it can absorb moisture and change dimensions. Density also matters. A lightweight
PC component may reduce shipping weight, while a denser plastic can improve stiffness and handling. These trade-offs are easy to underestimate.
Tips:
Request test data at the intended temperature and humidity. Use ISO 2768 only when general tolerances suit the design. It does not replace critical dimensions on a drawing. Check wall thickness, machining direction, and post-machining inspection requirements with the supplier. A practical material table should include tensile strength, HDT, density, moisture behavior, and tolerance capability. No material wins every test. My own selection reviews sometimes reveal that a cheaper plastic performs better after load testing, but only when the design is adjusted carefully.
Compare ABS, PC, and HDPE by Typical Tensile Strength and Cost
For global CNC buyers, seven practical plastic choices are ABS, polycarbonate (PC), HDPE, nylon, acetal, polypropylene, and PEEK. Based on typical ASTM D638 test data summarized by MatWeb, ABS commonly reaches 35–50 MPa tensile strength. PC usually measures 55–75 MPa, while HDPE remains around 20–35 MPa. These figures describe molded materials, not every machined grade.
Cost changes the decision quickly. Recent resin pricing reports from Plastics News and regional distributor quotations place standard ABS near USD 3–8 per kilogram, HDPE around USD 2–6, and PC near USD 5–12. Nylon and acetal often cost USD 6–16, while PEEK can exceed USD 80 per kilogram. PEEK is strong, but it may be unnecessary for a low-load cover.
Think about the finished part. ABS machines easily and suits housings, but it can soften near heat sources. PC handles impact better, though its internal stress may cause cracking during machining. HDPE is affordable and chemically resistant, yet its lower stiffness can produce flexible edges. Nylon offers strength, but moisture changes its dimensions. Acetal gives clean tolerances, while polypropylene is useful for lightweight chemical-contact parts. PEEK supports demanding temperatures, with a severe price penalty. These ranges are only guides. Stock thickness, machining waste, region, and order volume can change the final cost substantially. Tensile strength alone is an imperfect buying rule.
Assess POM and Nylon: 40–90 MPa Strength, Wear, and Moisture Effects
Choosing between POM and nylon requires more than comparing headline tensile strength. ISO 527-based data in the CAMPUS plastics database places common POM grades near 60–75 MPa. Dry nylon often reaches 65–90 MPa, depending on grade and reinforcement. These figures are not permanent. Nylon can lose stiffness after absorbing moisture. POM usually absorbs far less, often below 0.3% water uptake under ISO 62 testing. Nylon may approach 2–3% at equilibrium, especially in humid service.
That difference appears on the CNC bench. A nylon bushing may machine smoothly on Monday, then expand slightly after warehouse storage. POM holds dimensions more reliably. It also offers low friction and strong sliding wear performance in many unlubricated parts. Nylon can outperform it when impact resistance matters. Published tribology datasets show that wear depends heavily on load, speed, counterface, and lubrication, not material name alone. Keep that warning visible.
For shafts, guides, and tight-fit gears, I would validate moisture conditioning before production. Measure parts after 24 hours and again after several days. It is slower. It prevents expensive surprises. My practical mistake was trusting dry tensile data for a humid application. A small clearance change can become a seized assembly. Use ISO 527 for strength, ISO 62 for absorption, and application-specific wear testing before approving global batches.
7 Best CNC Plastic Materials for Global Buyers: POM and Nylon Strength, Wear, and Moisture Effects
Representative tensile-strength values compare dry and moisture-conditioned performance. Nylon generally loses more strength after moisture uptake, while POM, PEEK, PTFE, and UHMW-PE offer more stable dimensional behavior. Wear performance also depends on load, speed, temperature, surface finish, and whether the grade is reinforced.
Values are typical engineering ranges for unfilled CNC-machinable grades. Tensile strength is shown in MPa; moisture absorption is an approximate percentage at room temperature and moderate relative humidity. Actual results vary by grade, processing direction, conditioning, and test standard.
Specify PTFE and PEEK: 20–100 MPa Strength and 150–260°C Service Heat
Choosing CNC plastic is a performance decision, not merely a price comparison. PTFE and PEEK cover demanding applications where heat, friction, and chemical exposure matter. Typical tensile strength ranges from about 20 MPa for PTFE to nearly 100 MPa for reinforced or high-grade PEEK. Actual values depend on grade, temperature, wall thickness, and test direction.
PTFE
suits low-friction seals, sliding guides, and chemically aggressive environments. Its service temperature can approach 260°C, but sustained load may cause creep and dimensional movement. I have seen a tight PTFE fit loosen after repeated heating cycles. That detail is easy to miss.
PEEK
generally offers higher stiffness and strength, with continuous service commonly around 150–260°C, depending on formulation and load. It works well for precision bushings, electrical parts, and structural components near heat sources.
Machining both materials requires restraint. PTFE can deform under clamping pressure, while PEEK may develop heat-related distortion if chips remain trapped. Use sharp tools, controlled feeds, and generous chip clearance. Avoid assuming that a catalog value equals field performance. Request the material grade, test method, and temperature conditions from the supplier. Prototype critical parts and measure them after thermal cycling. A 100 MPa figure may look impressive, yet it can mislead without creep data and real load calculations. Specification discipline matters more than attractive numbers.
Validate Global Purchases with ASTM/ISO Grades, Tolerances, and COAs
Global CNC buyers often choose POM, PA, PEEK, PTFE, UHMW-PE, ABS, or PC plastics. The correct choice depends on load, temperature, moisture, friction, and machining stability. Do not approve a material from a trade description alone. Request the exact resin grade and its applicable ASTM or ISO reference. Standards can vary by composition, reinforcement, and testing method.
A reliable COA should identify the production batch, material grade, test date, and measured results. Check density, tensile strength, hardness, moisture, and reinforcement content when relevant. Ask whether the values are typical or actual batch results. That difference matters.
For dimensional control, define drawing tolerances before production. General CNC tolerances may not suit thin walls, deep pockets, or parts exposed to heat. Measure sample parts with calibrated equipment, preferably in a controlled environment. Plastic expands more than many buyers expect.
I have seen certificates that looked complete but lacked traceable lot numbers. That is a warning sign. Verify the COA against the packing label and purchase order. Keep inspection records, approved drawings, and retained samples together. For critical parts, request first-article inspection and independent testing. It costs more. Rework costs more. ASTM and ISO references improve communication, but they do not replace engineering judgment. A grade may pass the certificate and still fail after machining because of internal stress, warpage, or moisture absorption. Validate the material in the actual part design, not only on paper.